Stapling vs. Riveting vs. Clinching vs. Stitching vs. Welding
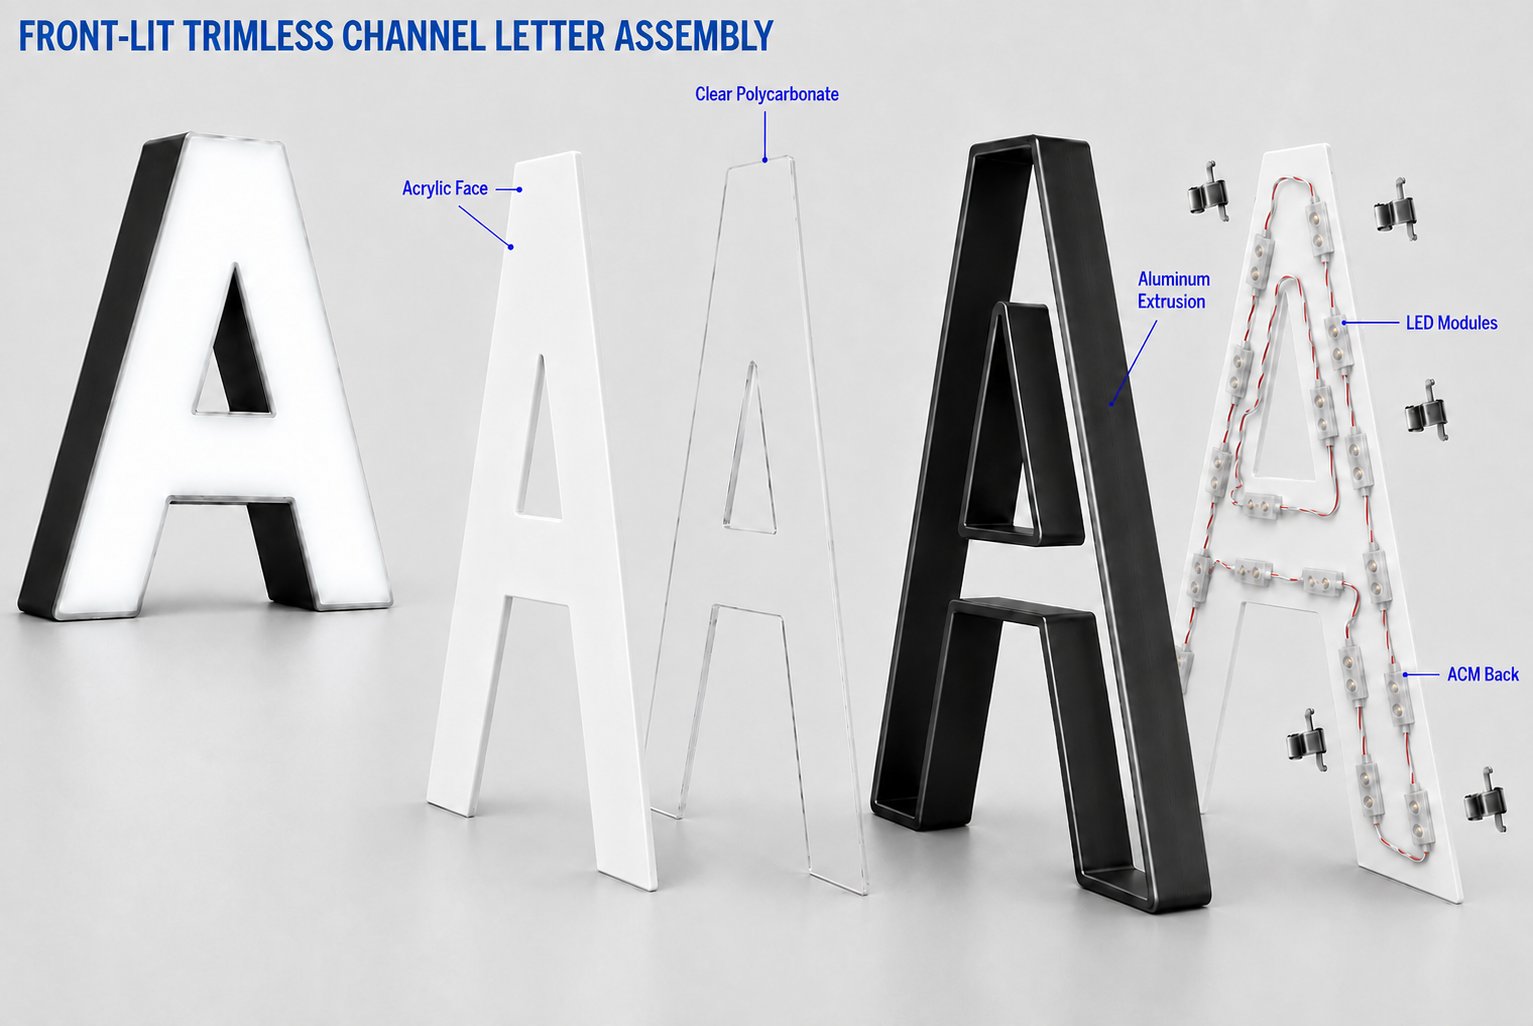
There's no single correct way to join a return to its face. Five methods show up across the sign industry, and each one trades off differently on material range, labor, appearance, and cost. Most shops end up using more than one, depending on the job in front of them. None of the five is a universal answer, including the stapler Ascent sells.
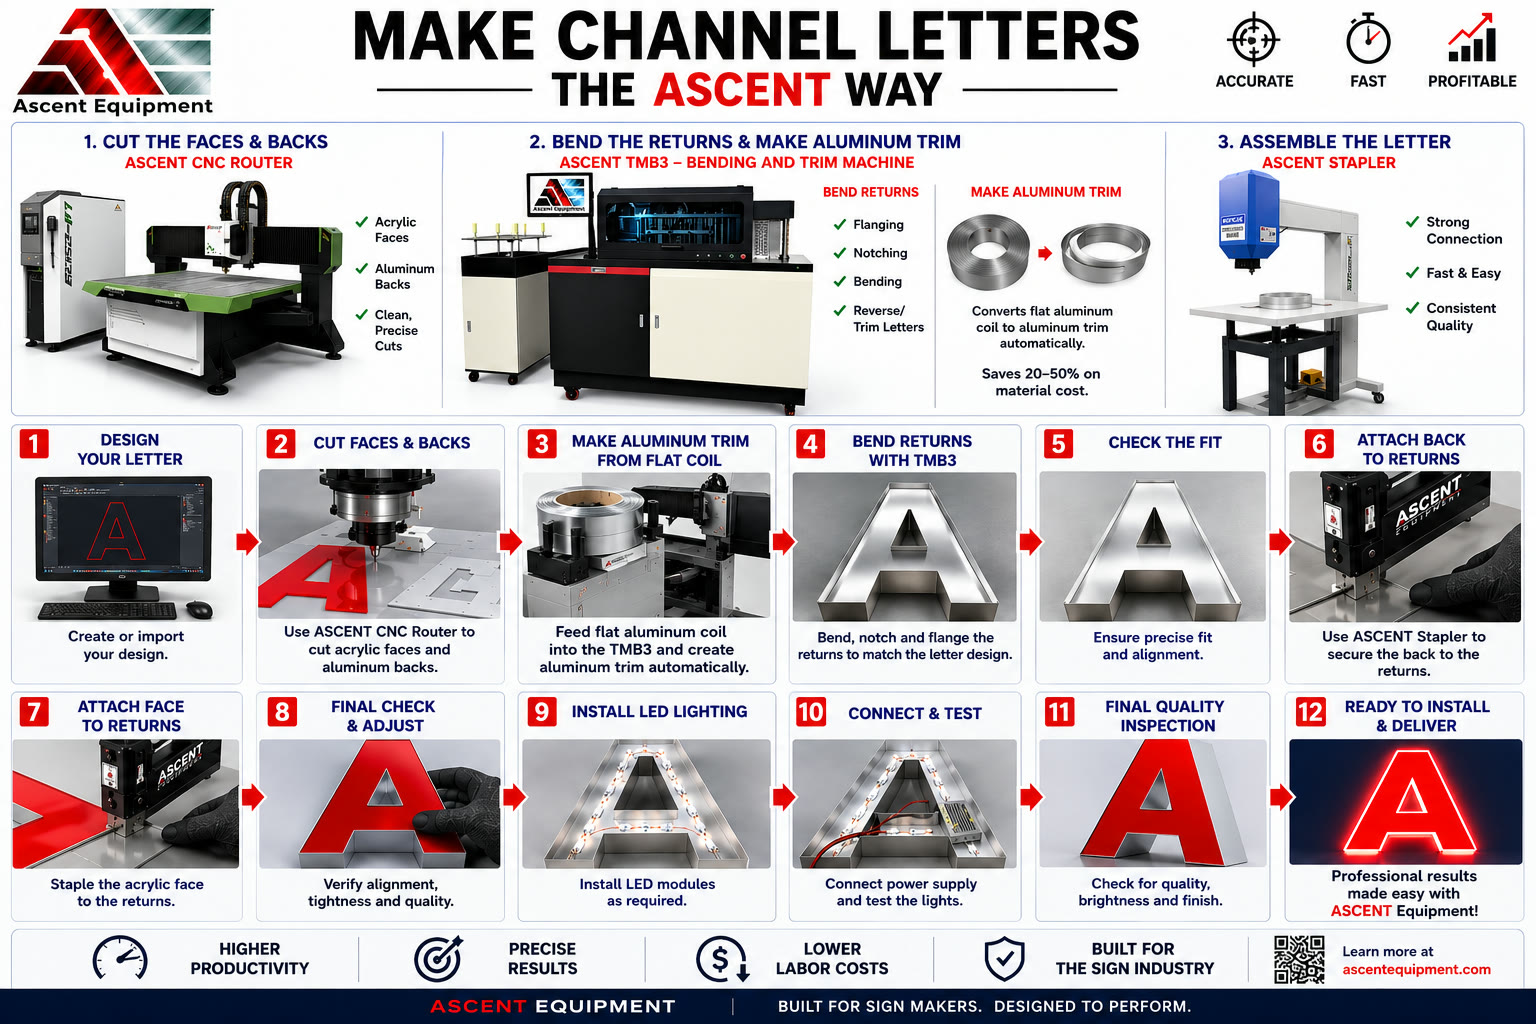
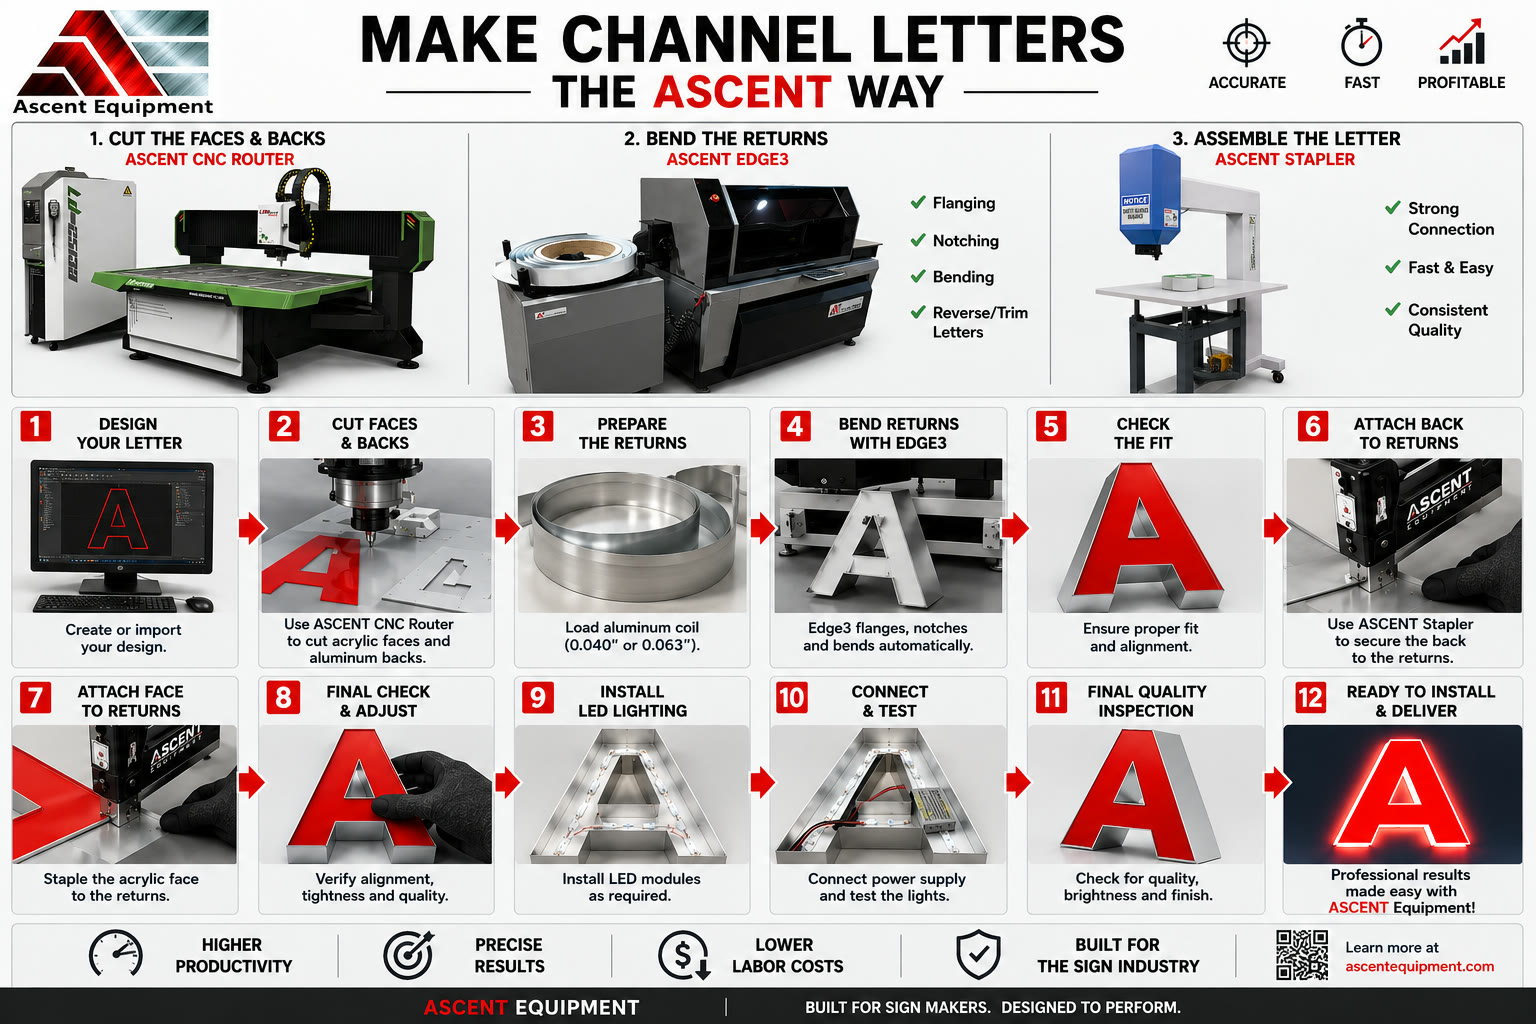
Stapling
Pneumatic stapling is fast and low-labor, and it works well on aluminum and thinner-gauge returns. It needs access from inside the letter, and the staples are a running consumable cost. It isn't the strongest join on thicker or heavier material — past a certain gauge, the staple has less to bite into and the join loses holding power.
Riveting
A solid mechanical join that covers a wider range of material thicknesses than stapling. It's slower per letter, since holes typically need to be drilled or punched first, and the rivets stay visible from the inside unless the interior is finished over.
Clinching
Clinching joins the material by deforming it, so there's no separate consumable at all: no staple or rivet to buy or run out of mid-job. It needs specific tooling and enough material overlap to form a clean joint, and it isn't a fit for every metal thickness.
Stitching
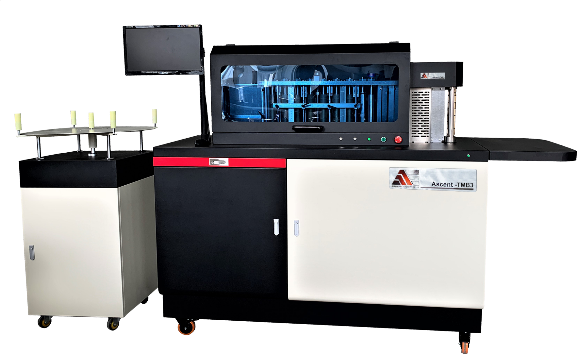
Channel-letter stitching machines feed 18-gauge wire from a coil and form their own staple at the joint, on aluminum, ACM (aluminum composite material), or polycarbonate, without predrilling. There's no pre-made staple to buy, one large coil is rated for tens of thousands of stitches, and a letter can be stitched in a minute or two. The catch is throat depth: these machines come in fixed sizes, a 13-inch throat for letters up to about 26 inches and a 26-inch throat for up to about 52 inches, so a larger or custom letter needs a support table. A stapler's table adjusts to the letter with no size limit built in.
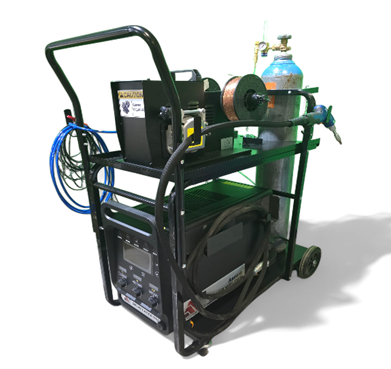
Welding
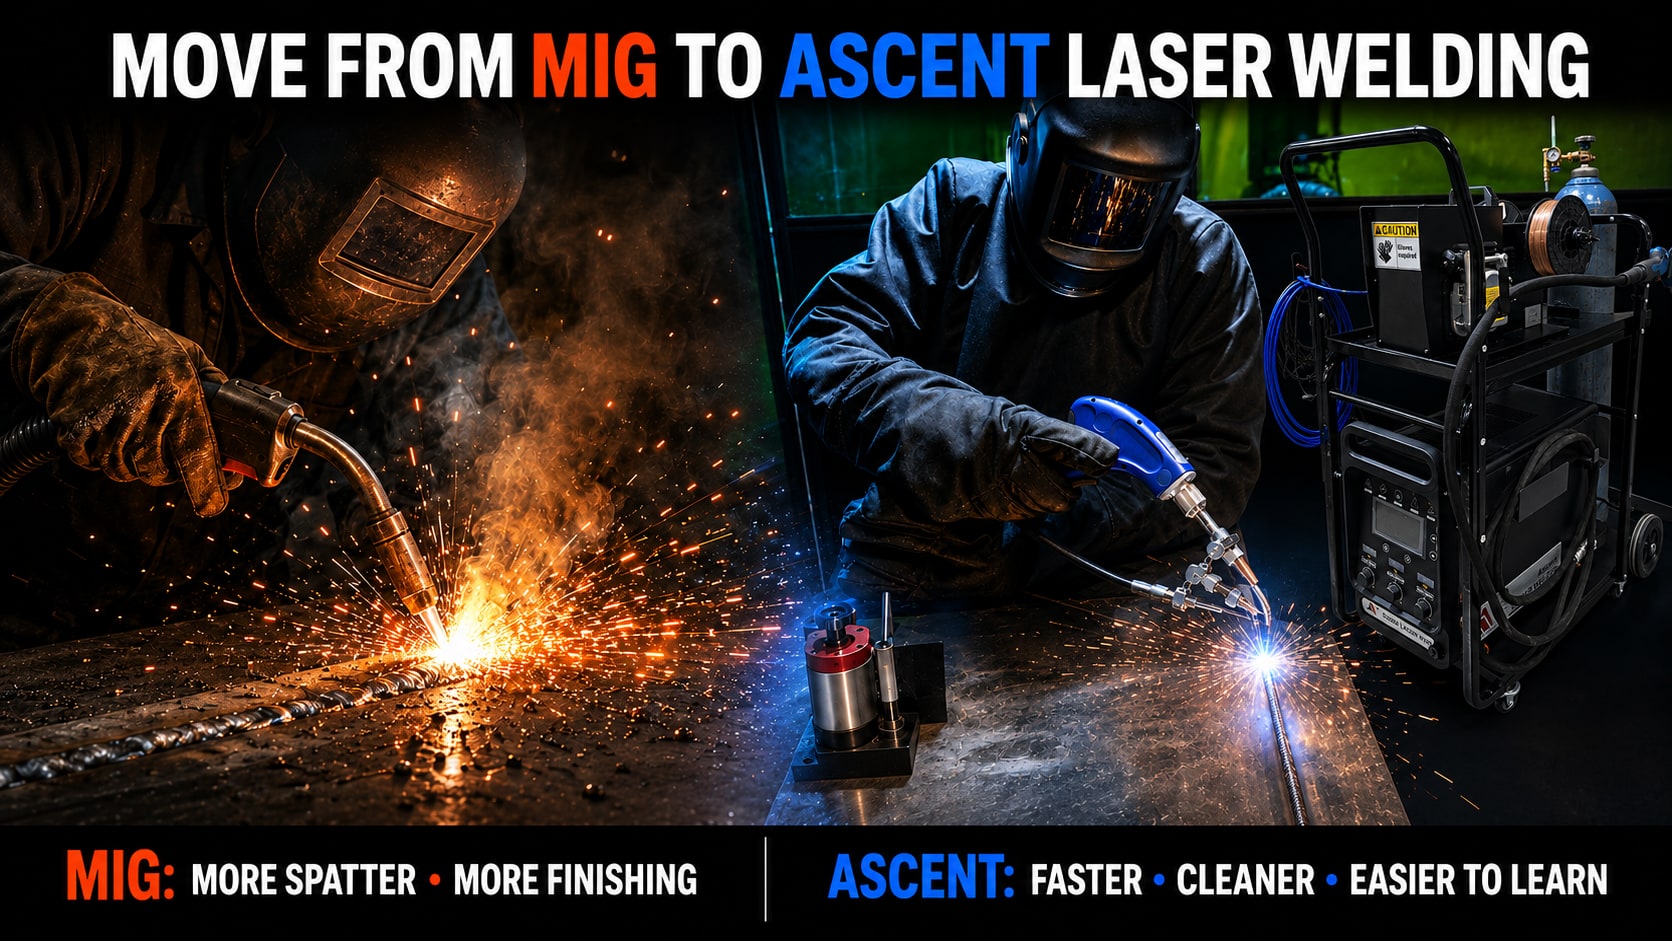
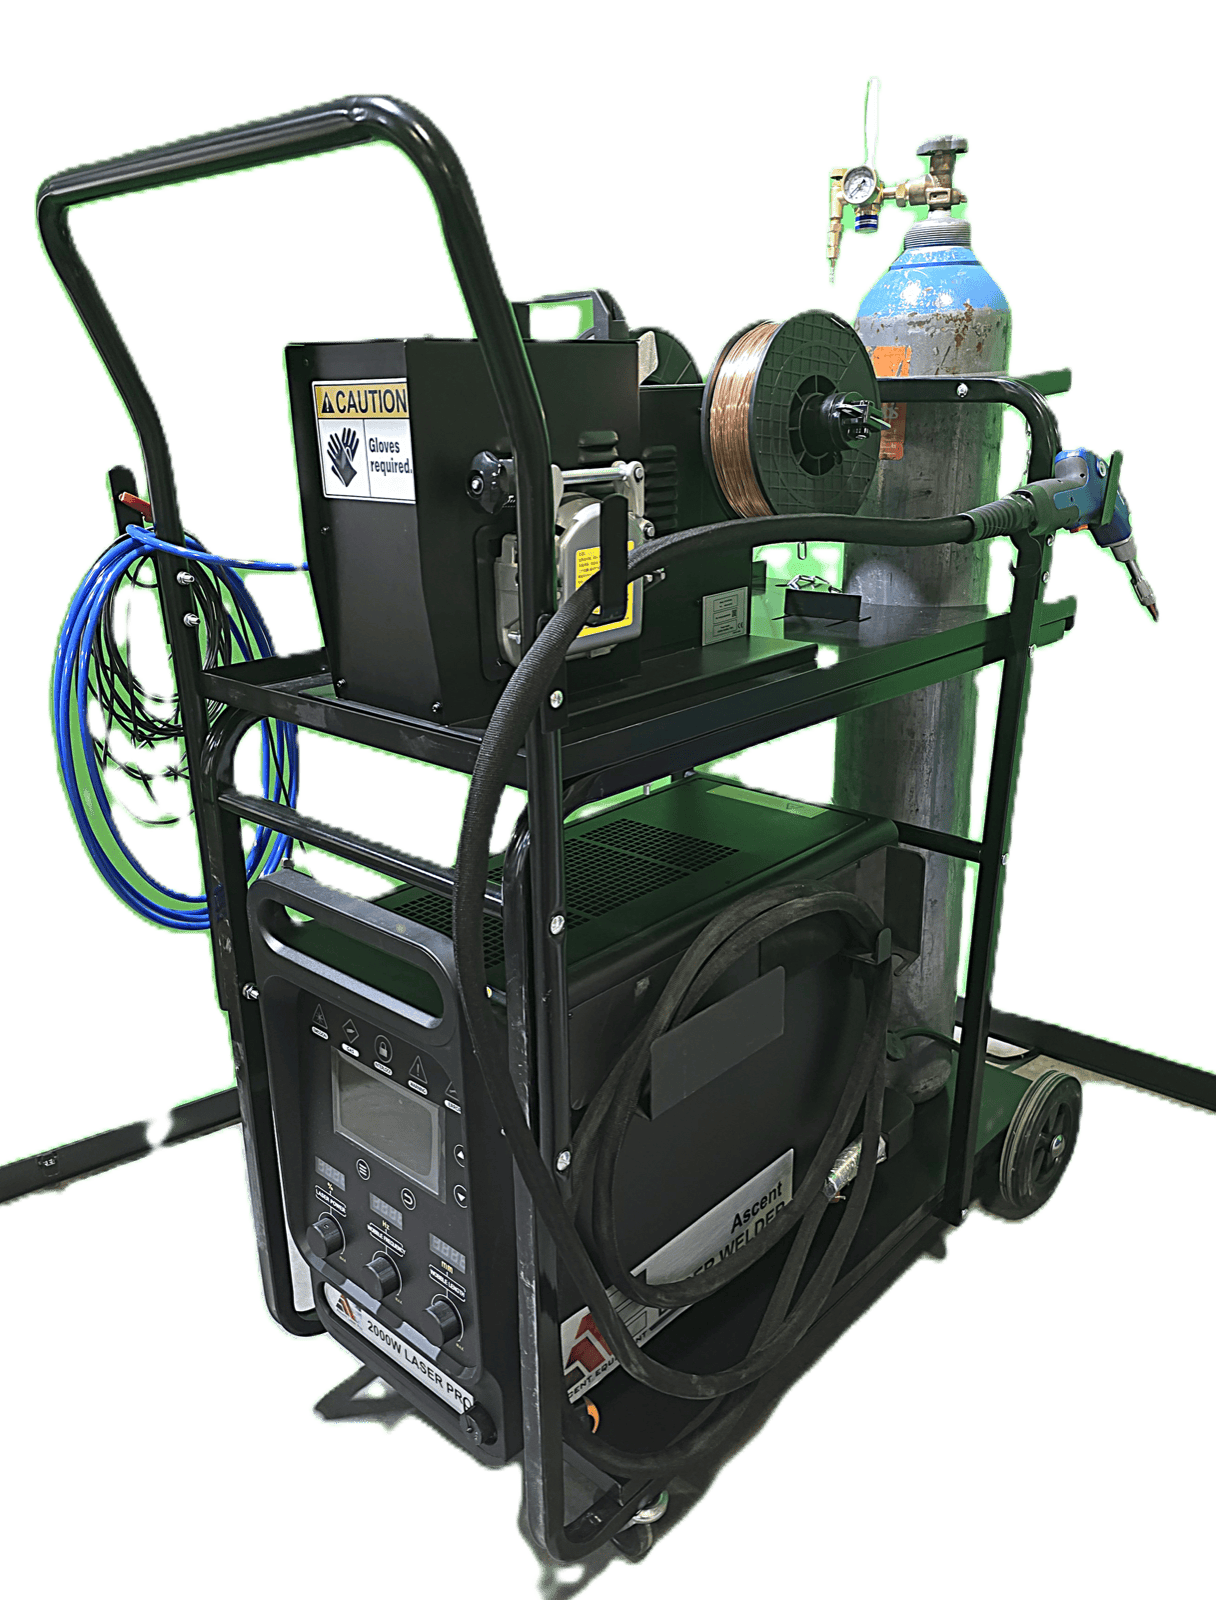
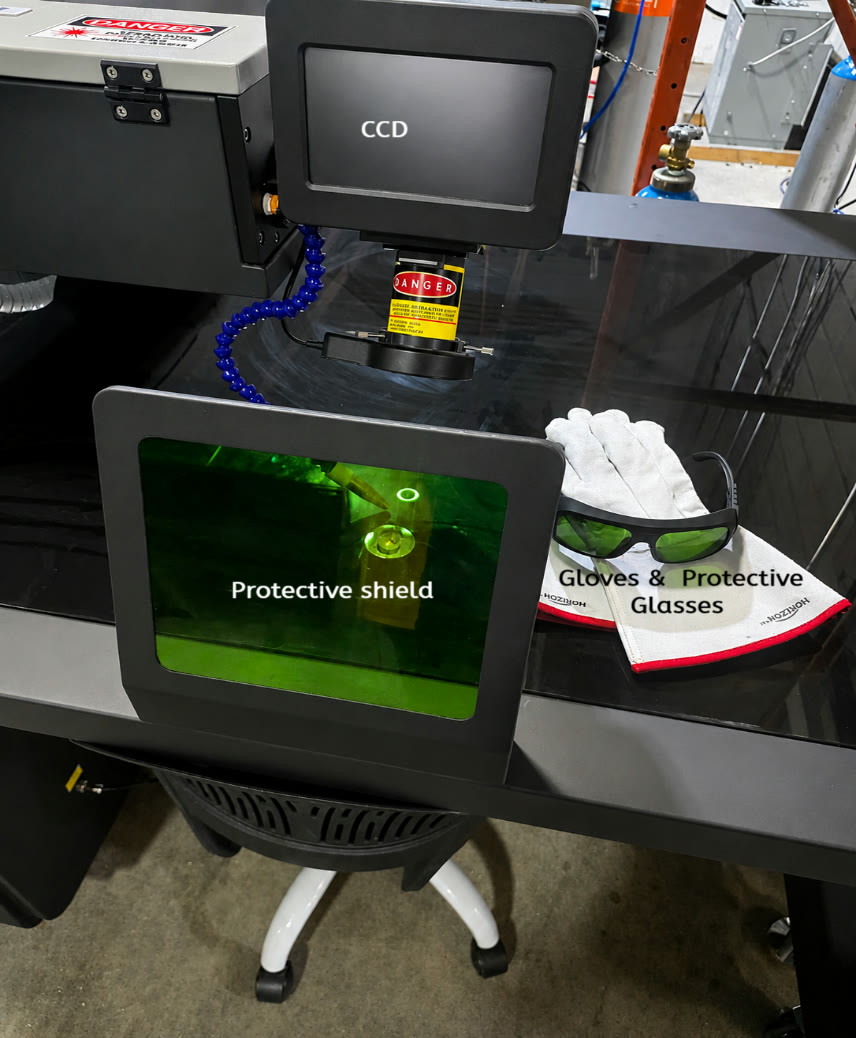
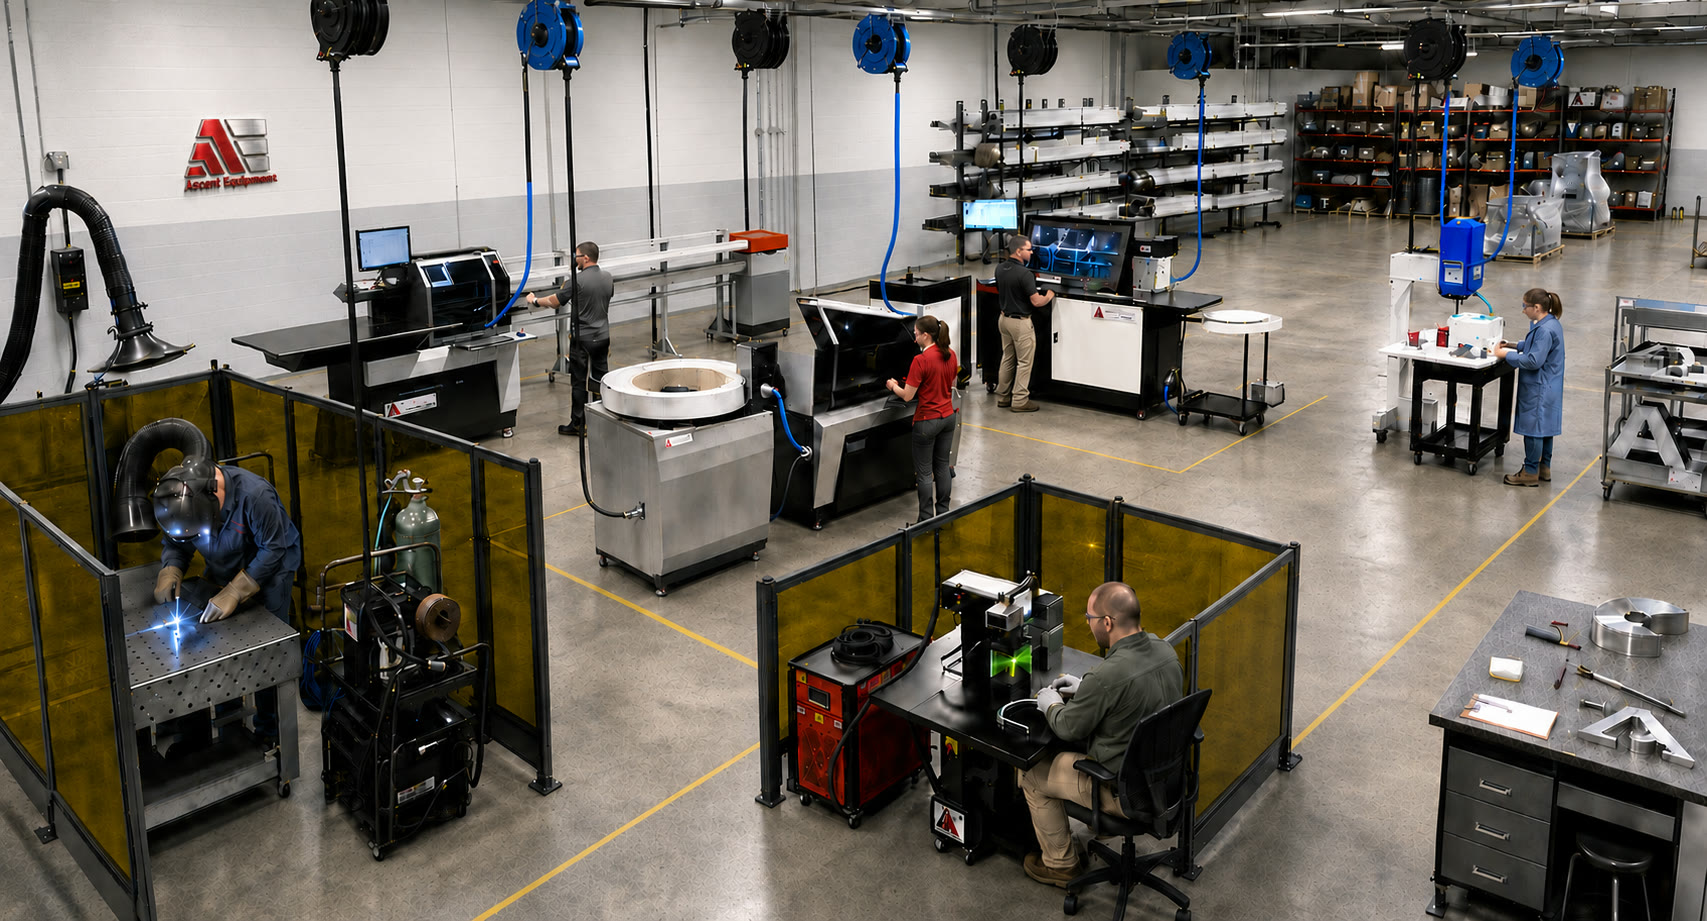
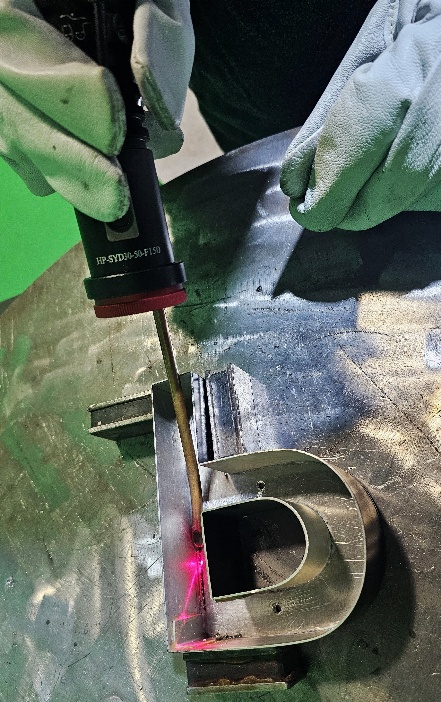
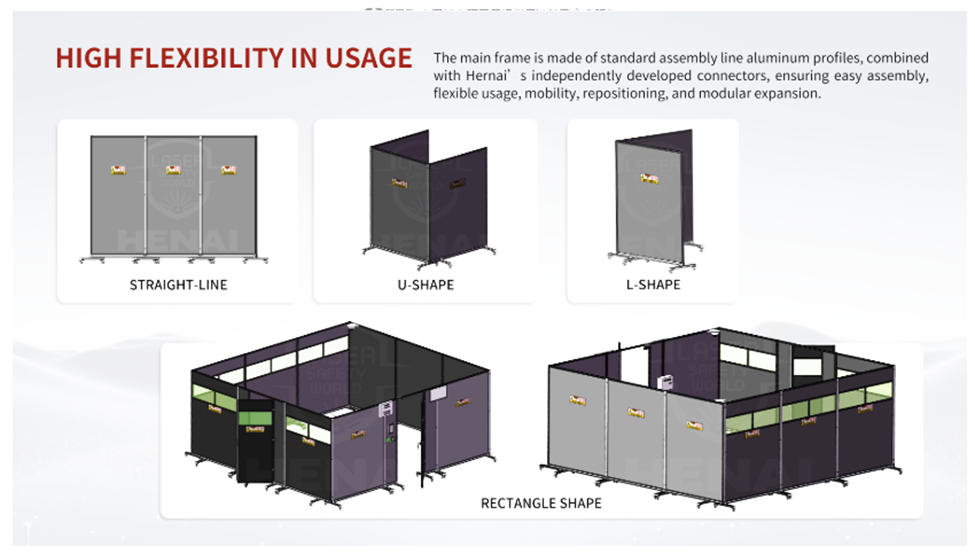
The strongest join of the five, and the only one that fully seals the seam. It's also the slowest and the most dependent on operator skill, and it needs the most safety infrastructure around it: ventilation, eye protection, and in some cases a dedicated enclosure. For returns that need to be watertight or structural, welding is often the only real option on this list.
Which One Fits Your Shop
Ascent's pneumatic stapler is built for the aluminum and lighter-gauge end of this range. It's a good fit for a lot of standard channel letter work, not a replacement for welding where the join has to be sealed or structural.
Against the three mechanical alternatives it competes with directly, here's Ascent's case. Against clinching: the stapler is safer to operate, connects ACM and polycarbonate backs as well as aluminum (clinching is metal-only), and costs less. Against self-piercing-rivet machines: a box of 5,000 staples runs about $40 (roughly $0.80 per 100) versus $35 per 100 rivets, and the stapler is cheaper to buy and easier to run. Against a stitcher: the stapler is safer around ACM and polycarbonate, its adjustable table is included in the price instead of sold separately, and it costs less and is easier to use.
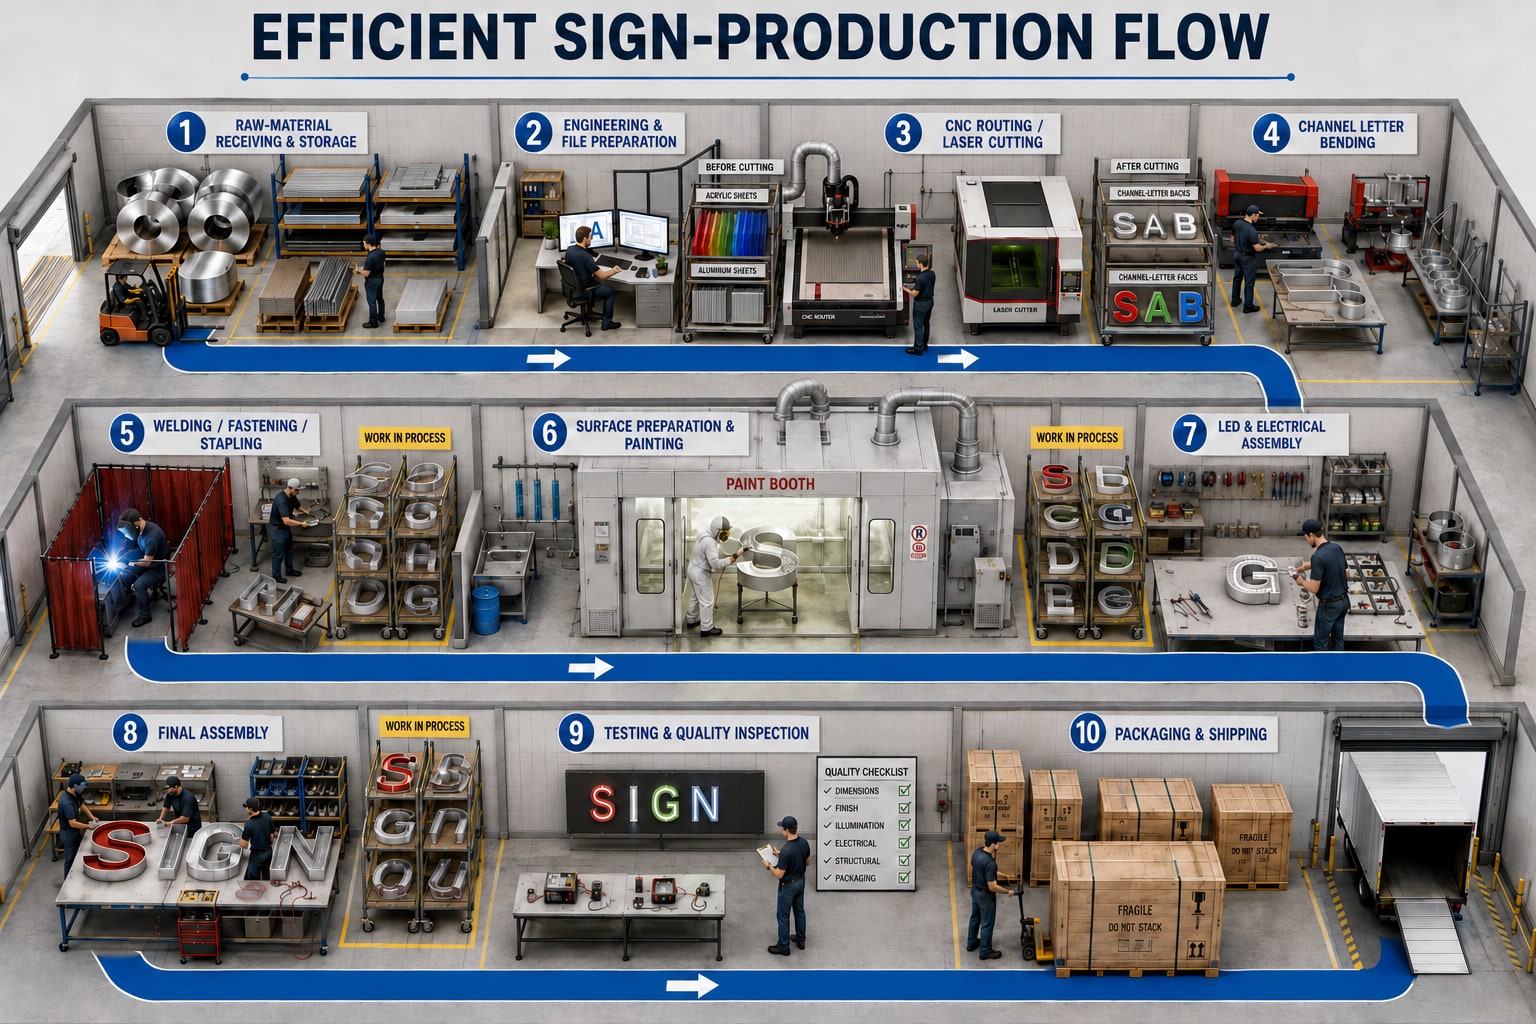
Before you standardize on one method, map it against the construction you actually build most often. Contact Ascent Equipment if you want to talk through which method, or which combination, fits your production mix.