How to Choose Your First Laser Welder
Shopping for a laser welder for the first time feels harder than it should be. Every spec sheet leads with wattage, every seller says theirs is the fastest, and it's not obvious which numbers actually matter for the job in front of you. Strip away the marketing and it comes down to a handful of real questions. Here's how to work through them.
Start With What You're Actually Welding
Power and cooling decisions only make sense once you know your material and thickness range. Aluminum, stainless, carbon steel, and mold-grade tool steel all behave differently under a laser, and mixed-metal work (aluminum to stainless, for instance) narrows your options further. Write down the thickest material you weld regularly — not the thickest you might someday weld — since that number drives almost every other decision on this list.
Match Power to the Job, Not the Spec Sheet
More wattage always sounds better, but it's not free: higher-power machines cost more to buy, draw more electrical service, and can be harder to control on thin material if you don't need the extra headroom. As a rough guide, a 1,500W fiber welder handles stainless up to roughly 7mm, a 2,000W unit gets you to about 9mm, and 3,000W pushes to around 12mm, with aluminum and carbon steel scaling proportionally. If your heaviest regular job is standard-gauge sheet metal, the middle tier is usually the right buy — the top tier is for shops doing genuinely heavy fabrication, not insurance against a job that might show up someday.
Handheld, Tabletop, or Fixed Precision?
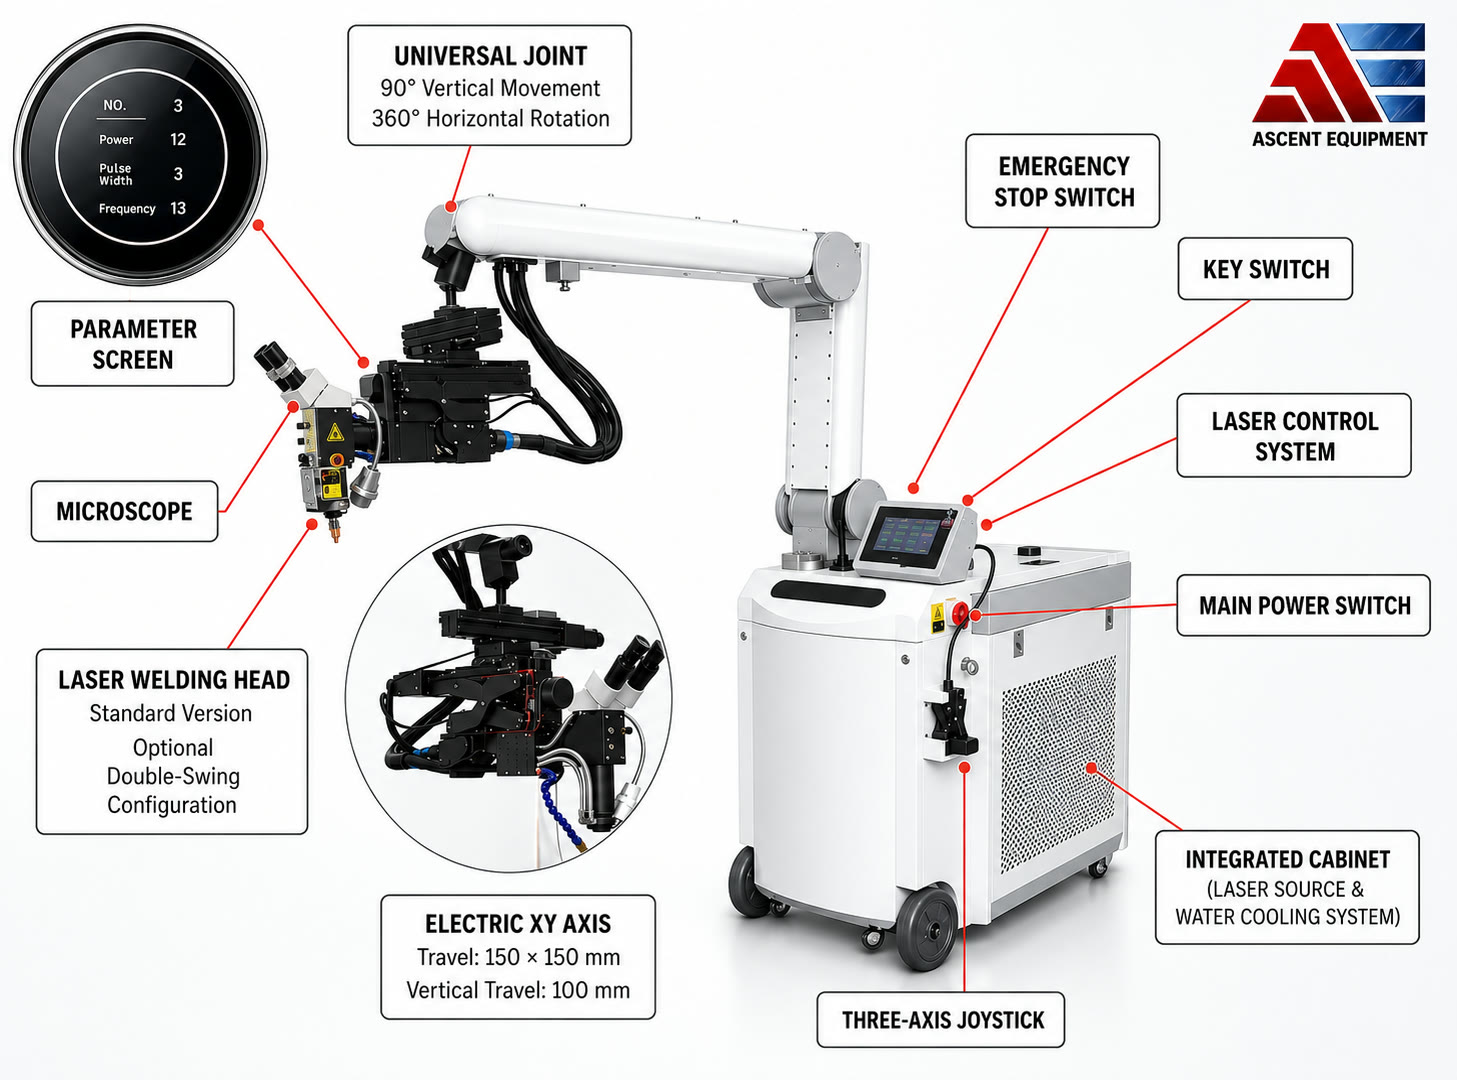
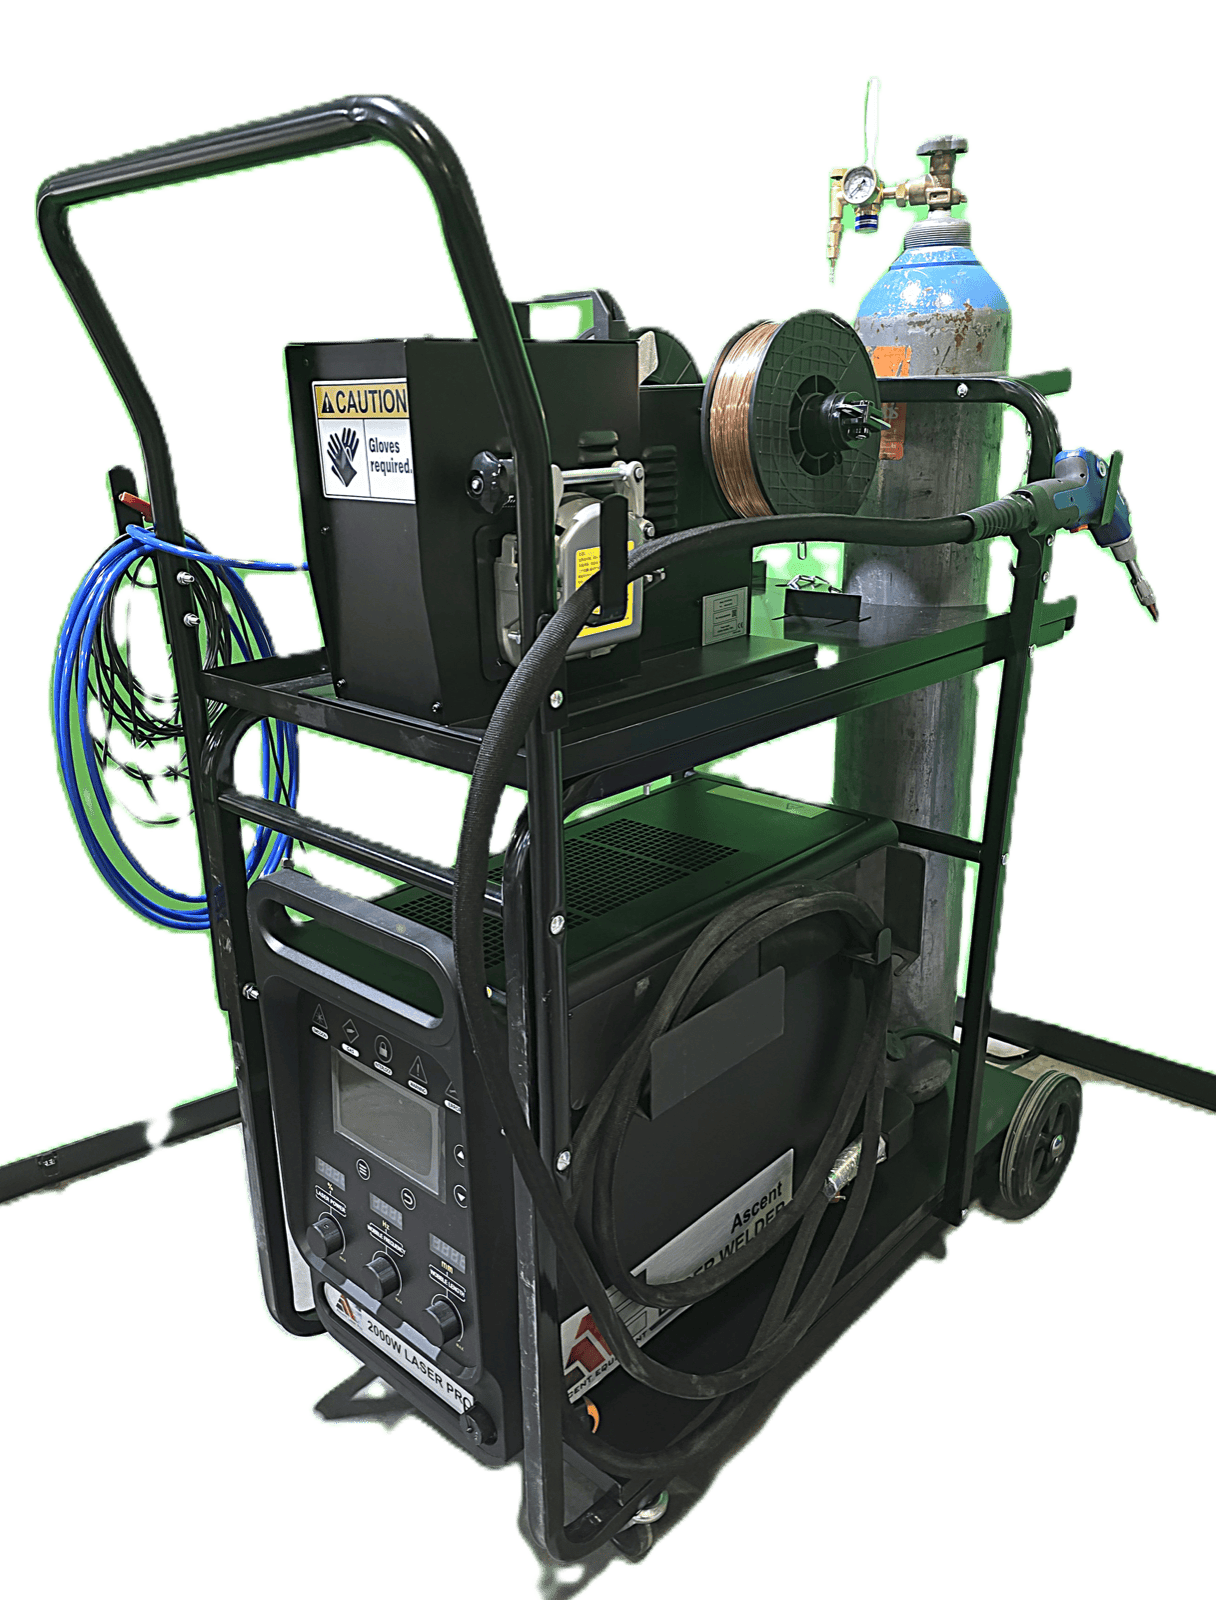
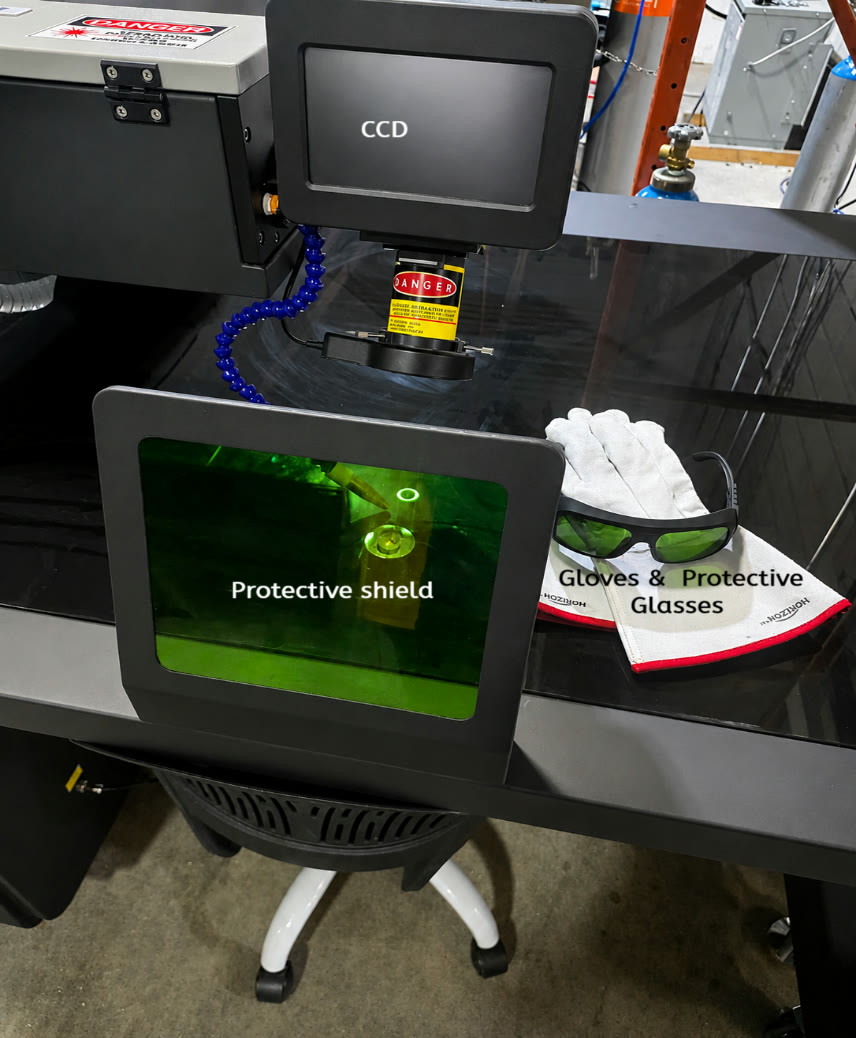
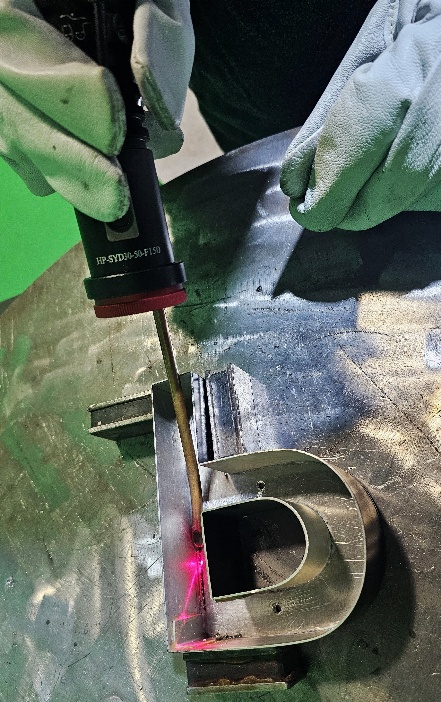
These aren't different power levels of the same tool — they're different tools for different work. A handheld torch goes wherever the part is, which matters for fabrication, assembly, and anything too large or oddly shaped to bring to a machine. A fixed tabletop system, working under a microscope or camera with an XY table, is built for the opposite problem: small, precise repairs where the part comes to the beam — mold and die repair, fine detail work, engraving corrections. Buying a handheld unit for tabletop-precision work, or a fixed system for shop-floor fabrication, is one of the most common first-purchase mistakes.
Pulsed (QCW) or Continuous Wave?
This decision shapes how much heat ends up in your part. A continuous-wave laser puts out steady power the whole time the beam is on, which is efficient for thicker material and faster bulk welding, but it pours more total heat into thin or heat-sensitive parts. A QCW (quasi-continuous-wave) laser delivers the same average power in short, intense pulses instead, so the peak power is far higher than the average rating while the part gets brief pauses to cool between pulses. That combination is what makes QCW the better choice for thin aluminum, small stainless sections, and anything where warping or discoloration is a real risk — and it's also what lets a modest average-power machine punch through the reflectivity of bright metals like copper and aluminum, since the instantaneous peak is what actually starts the weld pool.
How It's Cooled Matters More Than Most Buyers Expect
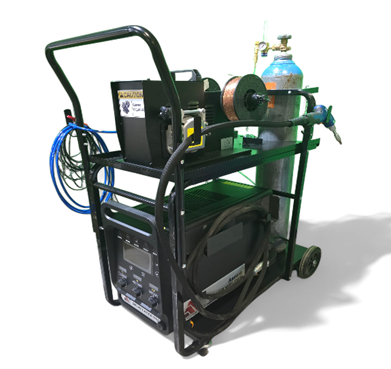
This is the factor that gets skipped in most buying guides, and it shouldn't be. Air-cooled machines are the simplest and cheapest, but they can't sustain high duty cycles — the laser throttles back or shuts down to avoid overheating during long runs. A water chiller solves that, but it's another system to maintain, another thing that can leak or freeze, and it adds real footprint. Refrigeration cooling (a sealed heat-pump loop, the same principle as an air conditioner rather than an open water circuit) is the newer option: it holds a 100% duty cycle across a wide temperature range with less maintenance than a chiller and no water lines to run. If continuous operation matters to your shop, ask specifically how a machine is cooled — "water-cooled" and "refrigeration-cooled" are often used loosely, and the difference shows up the first time you run it all day.
Budget for Safety Gear, Not Just the Machine
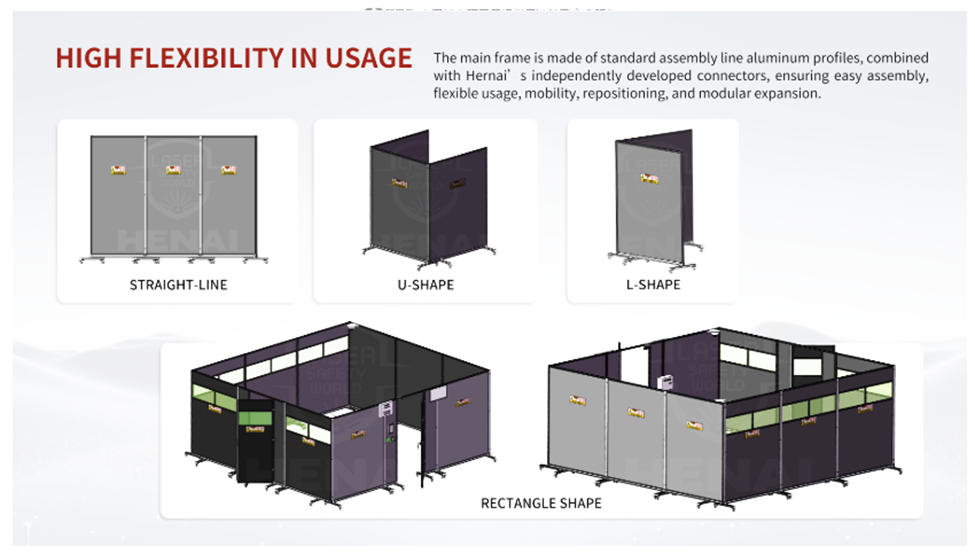
Every laser welder capable of doing real work is a Class 4 laser hazard, and that's true regardless of price point. Budget for OD-rated eyewear matched to the machine's actual wavelength (not generic "laser glasses"), a partition or enclosure around the work area, and — if you're setting up a dedicated room — a door interlock that cuts the beam when someone walks in. First-time buyers routinely spend their whole budget on the machine and treat safety gear as an afterthought; it should be priced in from the start, not added after the first near-miss.
Ask What the Quoted Price Actually Includes
A laser welder's sticker price rarely tells the whole story. Before comparing two quotes, check each one for the same things: Is installation included, or billed separately once the crate arrives? Is training on-site, or a video call? What's the warranty term, and does it cover labor or only parts? Is remote support included for the life of the machine, or a limited window? Two quotes that look close on the headline number can differ by thousands of dollars once freight, training, and warranty terms are actually spelled out — get everything in writing before you compare price tags.
The Short Version
Know your thickest regular material first. Buy the power tier that covers it with some margin, not the biggest number on the price list. Match the machine format — handheld or fixed — to where the work actually happens. Lean toward QCW if your material is thin, reflective, or heat-sensitive. Ask exactly how it's cooled and what a full quote actually includes. Get that right, and the rest of the decision gets a lot simpler.
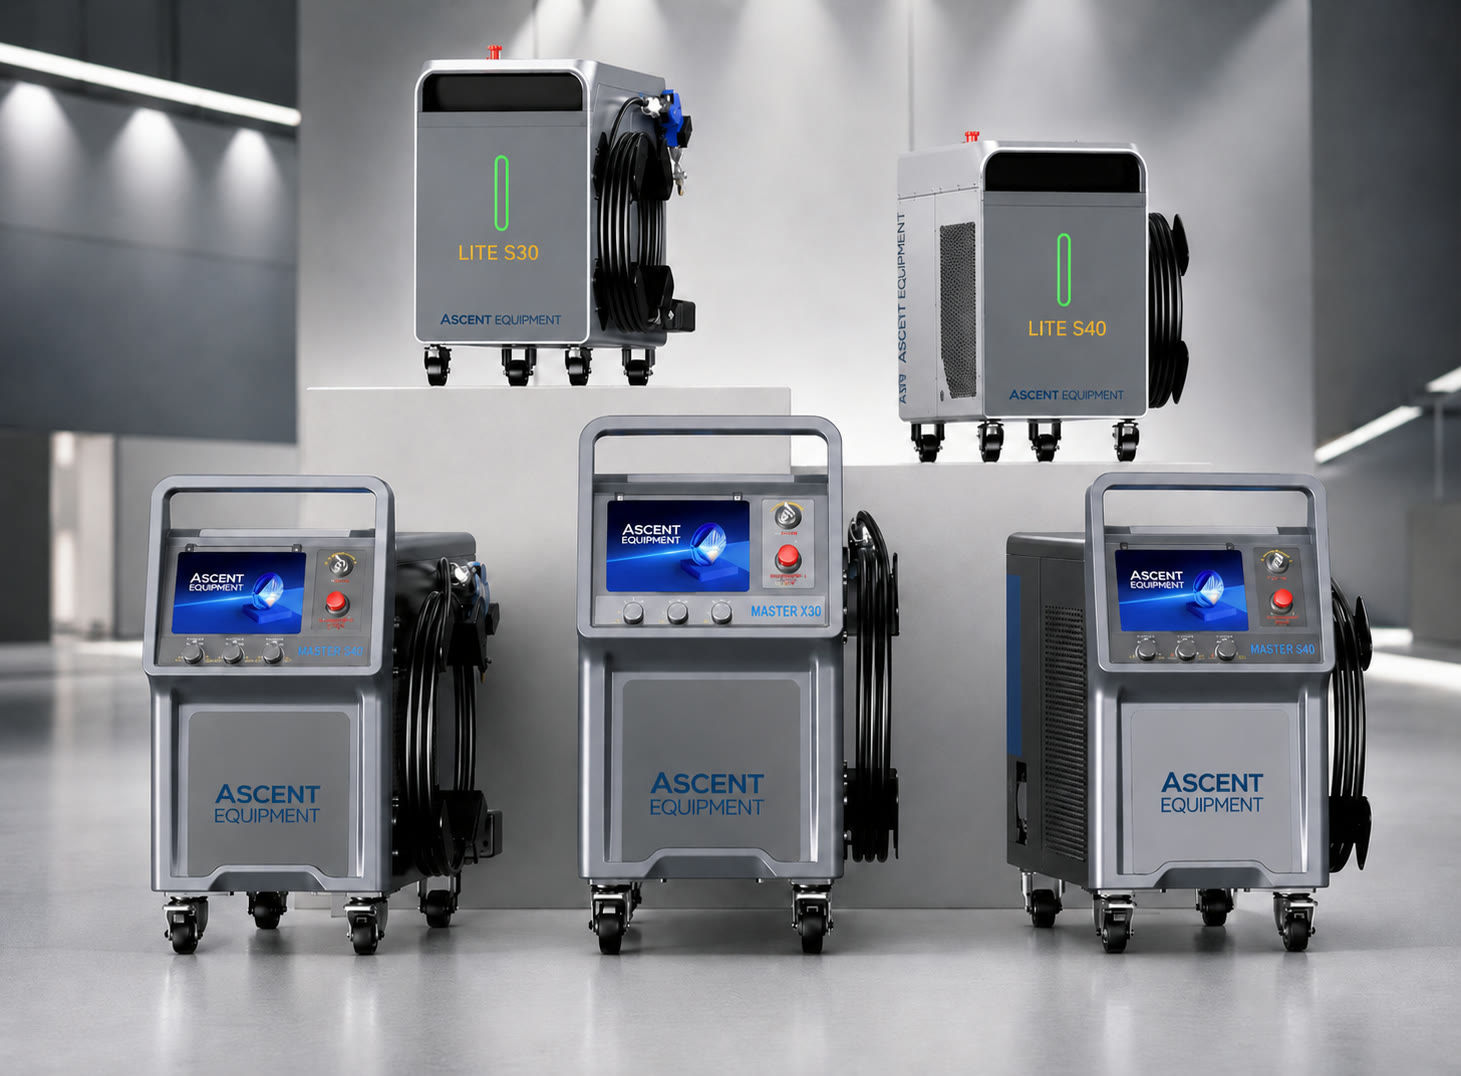
If you want to talk through which setup fits your shop, see Ascent's refrigeration-cooled handheld welders or the QCW tabletop system built for fine-detail work, and contact Ascent Equipment with your material and thickness and we'll help you land on the right one.