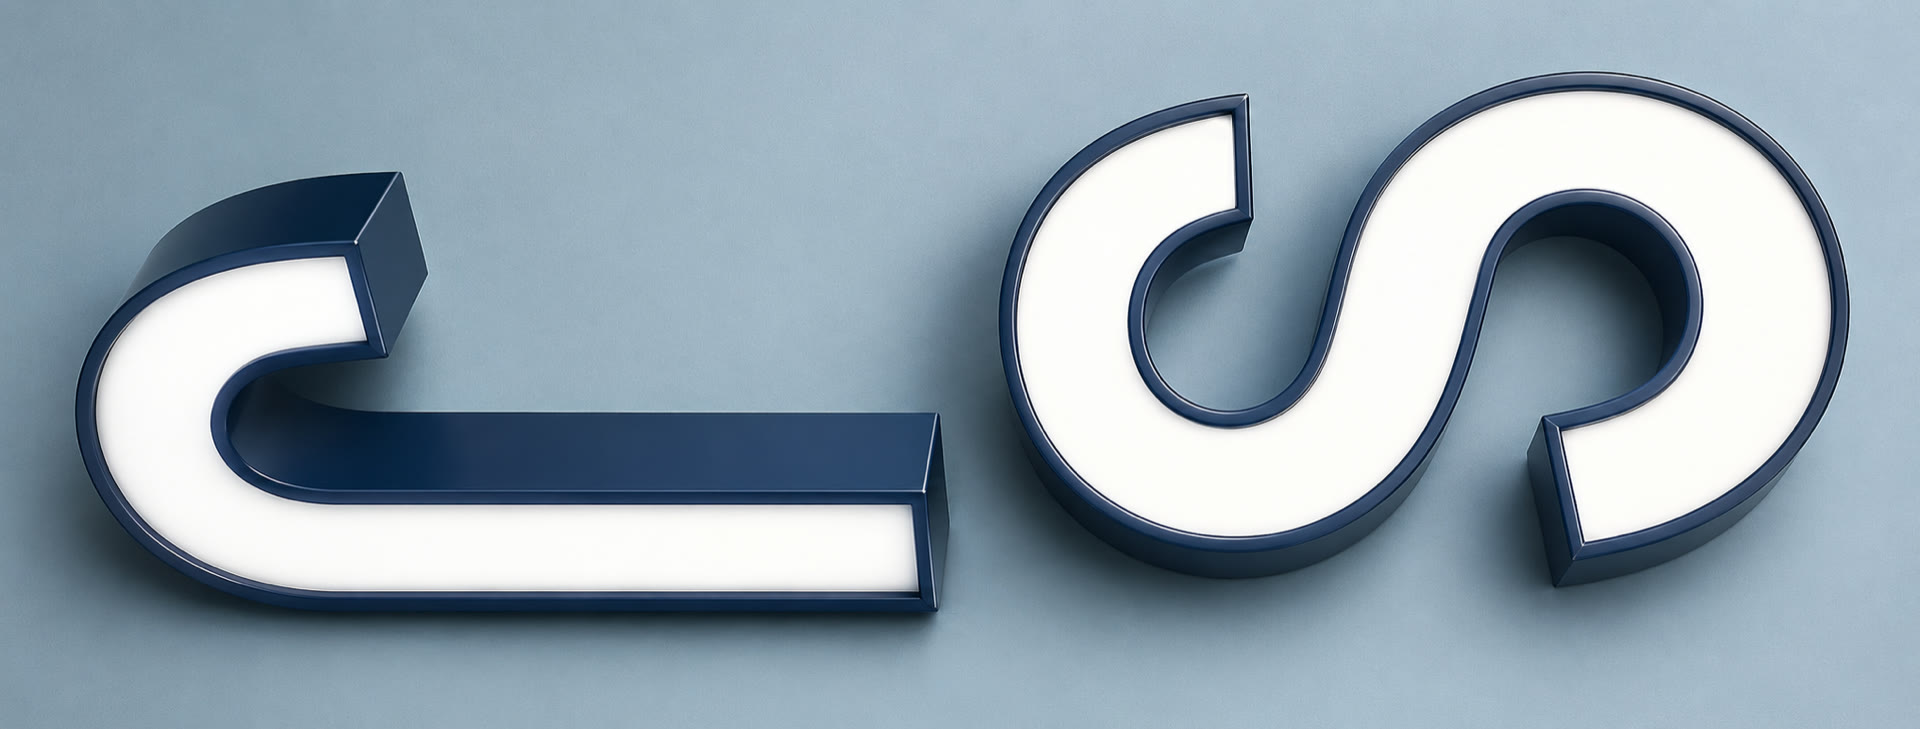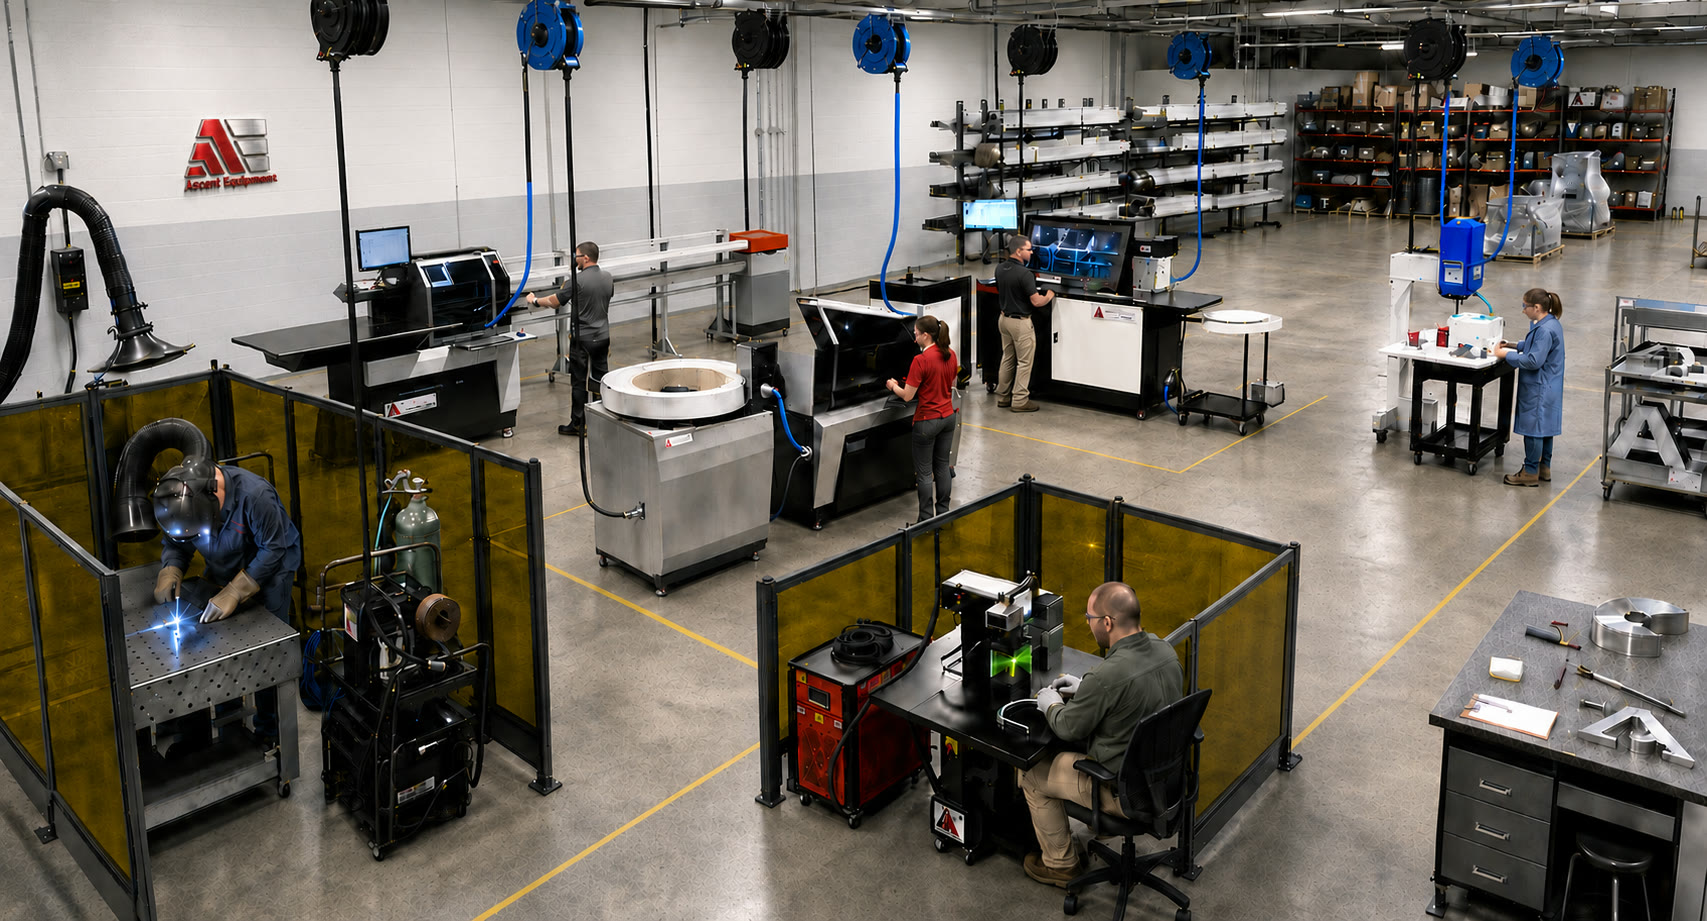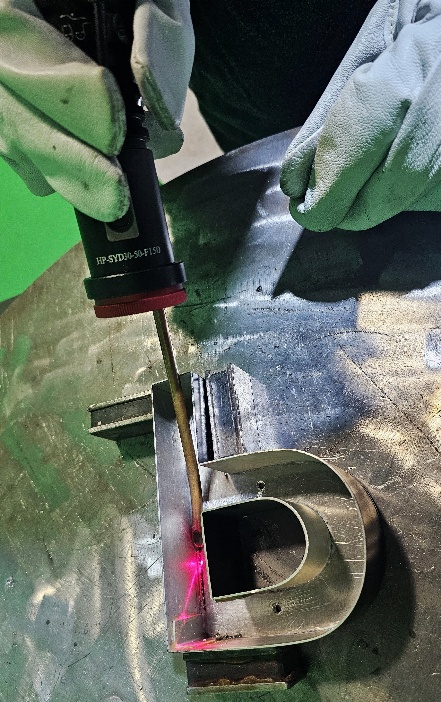
For shops cutting channel letter faces and backs every week, a 130W CO₂ laser is a practical step up from routing acrylic. It produces a clean edge, handles the thicknesses used on most letters, and does not require a larger production crew. Here is the workflow we teach shops using the Ascent Acrylic Laser Cutter.
Why CO₂ is the practical power level for channel letters
Most channel letters don't need extreme wattage. A well-tuned 130W Acrylic Laser Cutter delivers:
- Clean edges on cast and extruded acrylic for face and back panels.
- Useful speed for common thicknesses (e.g., 3–6 mm acrylic), so you're not waiting on parts.
- Low running complexity—fewer consumables than routers, no bits to replace after every long run.
- Compact footprint that suits small and mid-size shops in Canada & USA.
Look at how often you cut acrylic thicker than 10 mm. If the answer is rarely, 130W will usually cover the work without paying for power you seldom use.
What parts of a channel letter does the laser handle best?
Your 130W Acrylic Laser Cutter is perfect for:
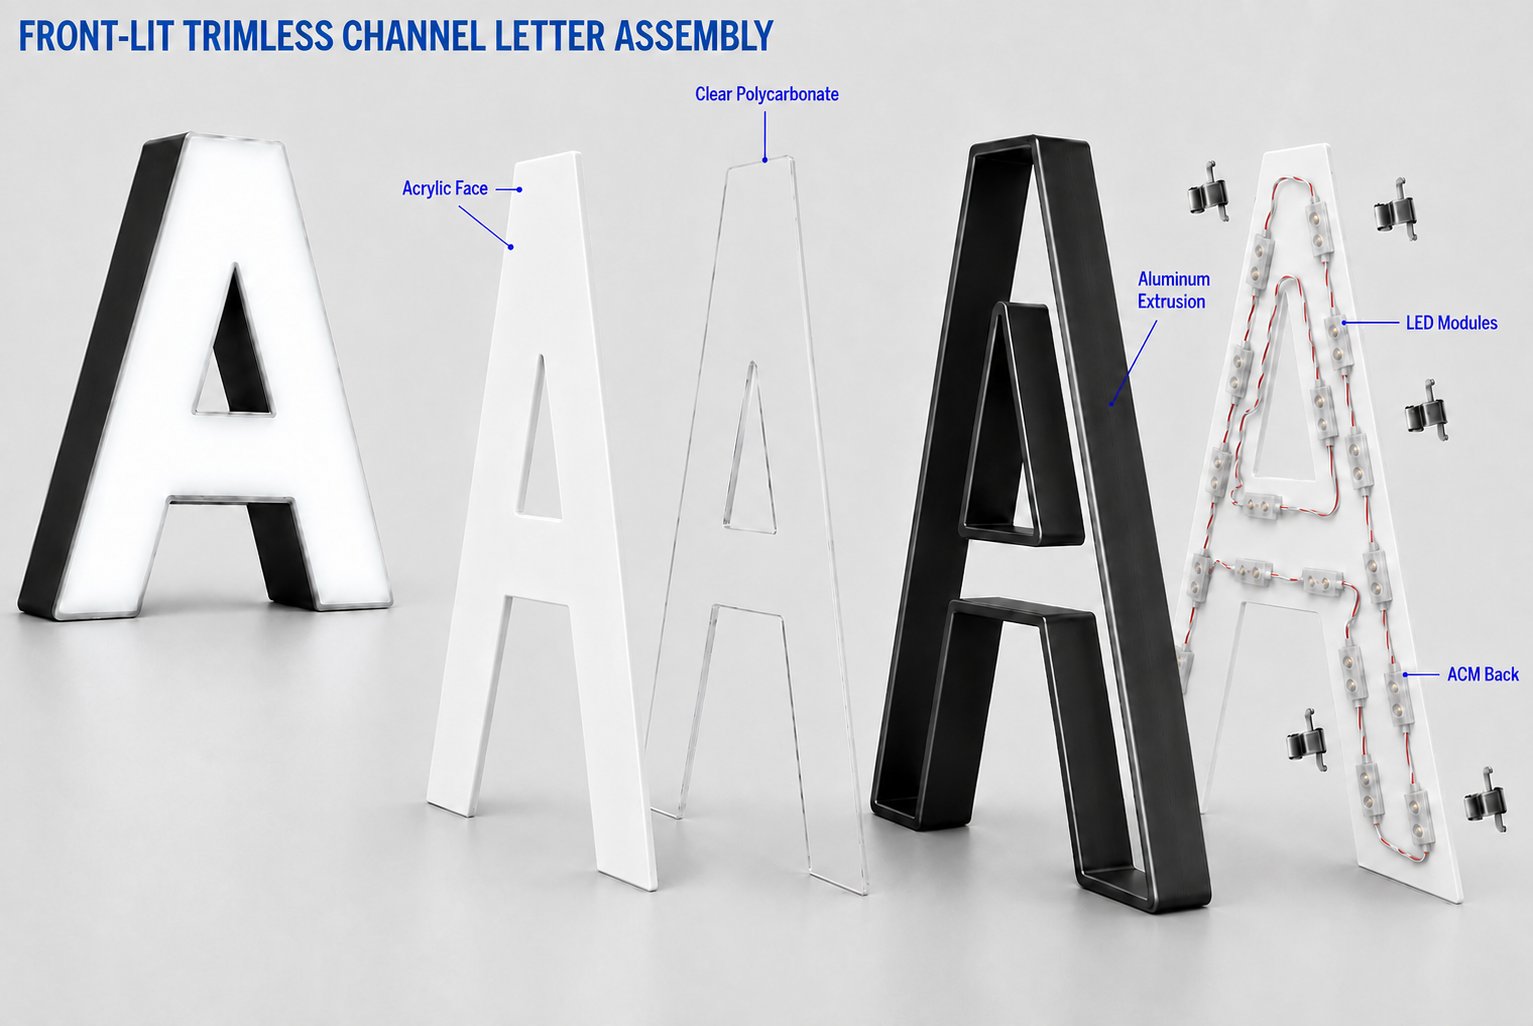
- Faces and backs (cast acrylic for crisp edges, extruded for budget work).
- Diffusers and light management layers (white acrylic or specialty plastics).
- Templates and jigs for assembling returns.
- Letter spacers, standoffs, and mounting guides cut from PVC sheet (where permitted).
For many shops in Canada & USA, the router still plays a role for thick substrates or metals, but the laser takes over for precision plastics:
- Tiny serifs and inner corners appear sharper than those of routered parts.
- Edge gloss can reduce post-processing (less flame polishing, fewer hand-finishing steps).
- Engrave-then-cut workflows (labels, serials, assembly marks) keep everything in one pass.
Include sanding and polishing time when you compare the laser with a router. That finishing time often drops sharply when faces and backs move to an Acrylic Laser Cutter.
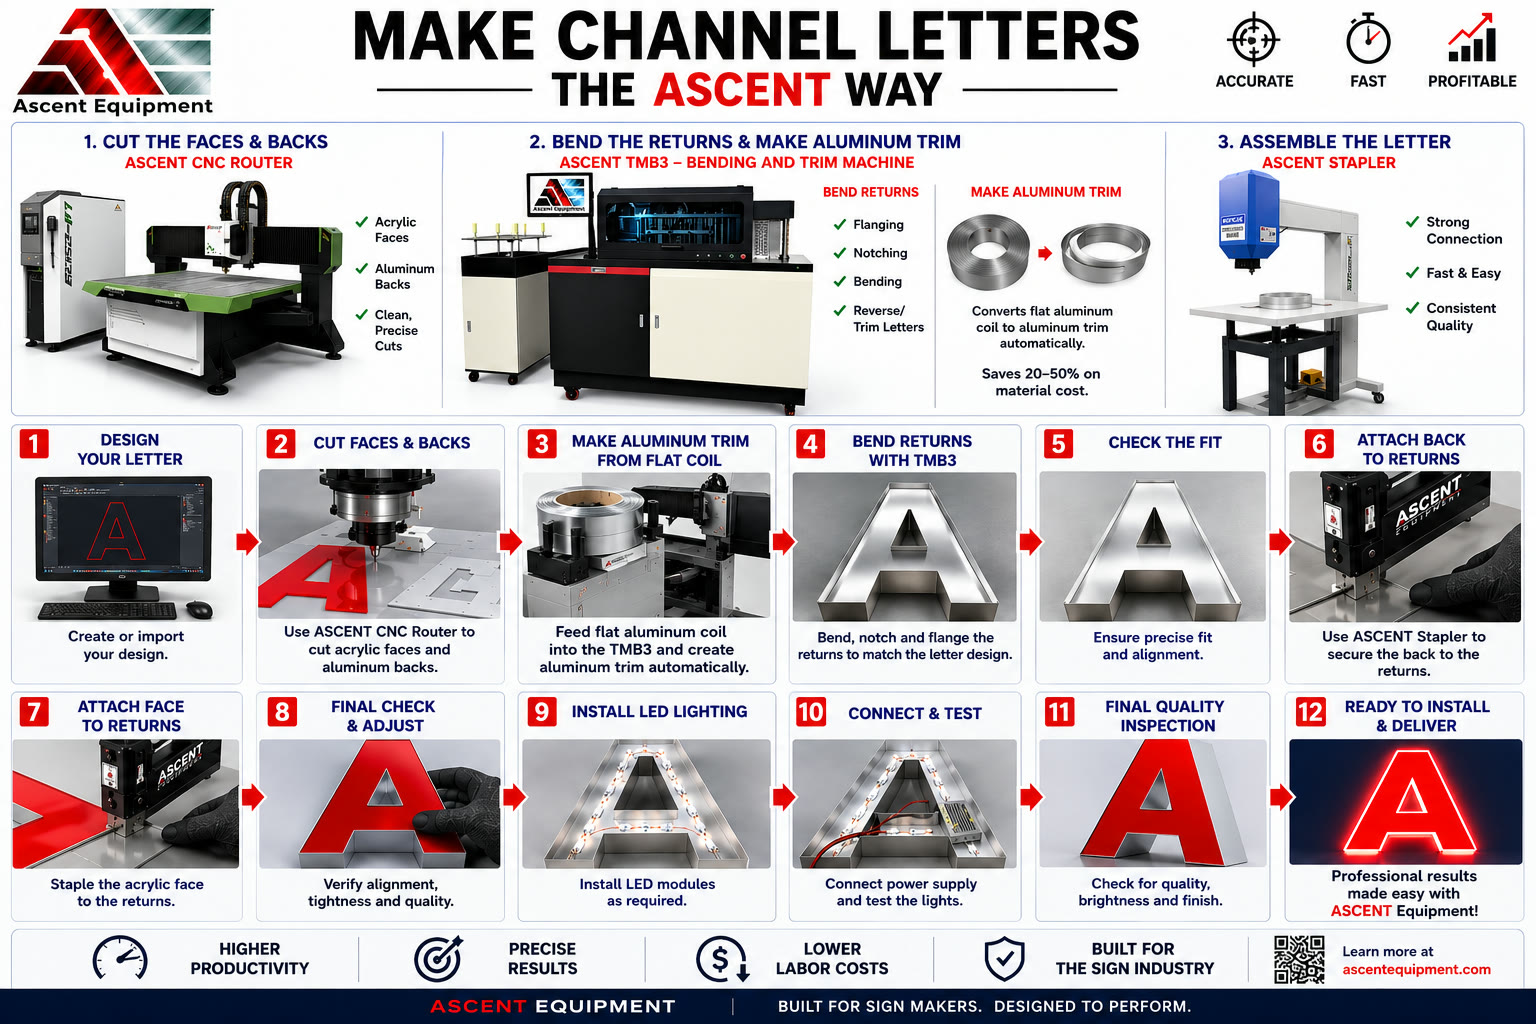
File-to-finish workflow that saves hours with our Acrylic Laser Cutter
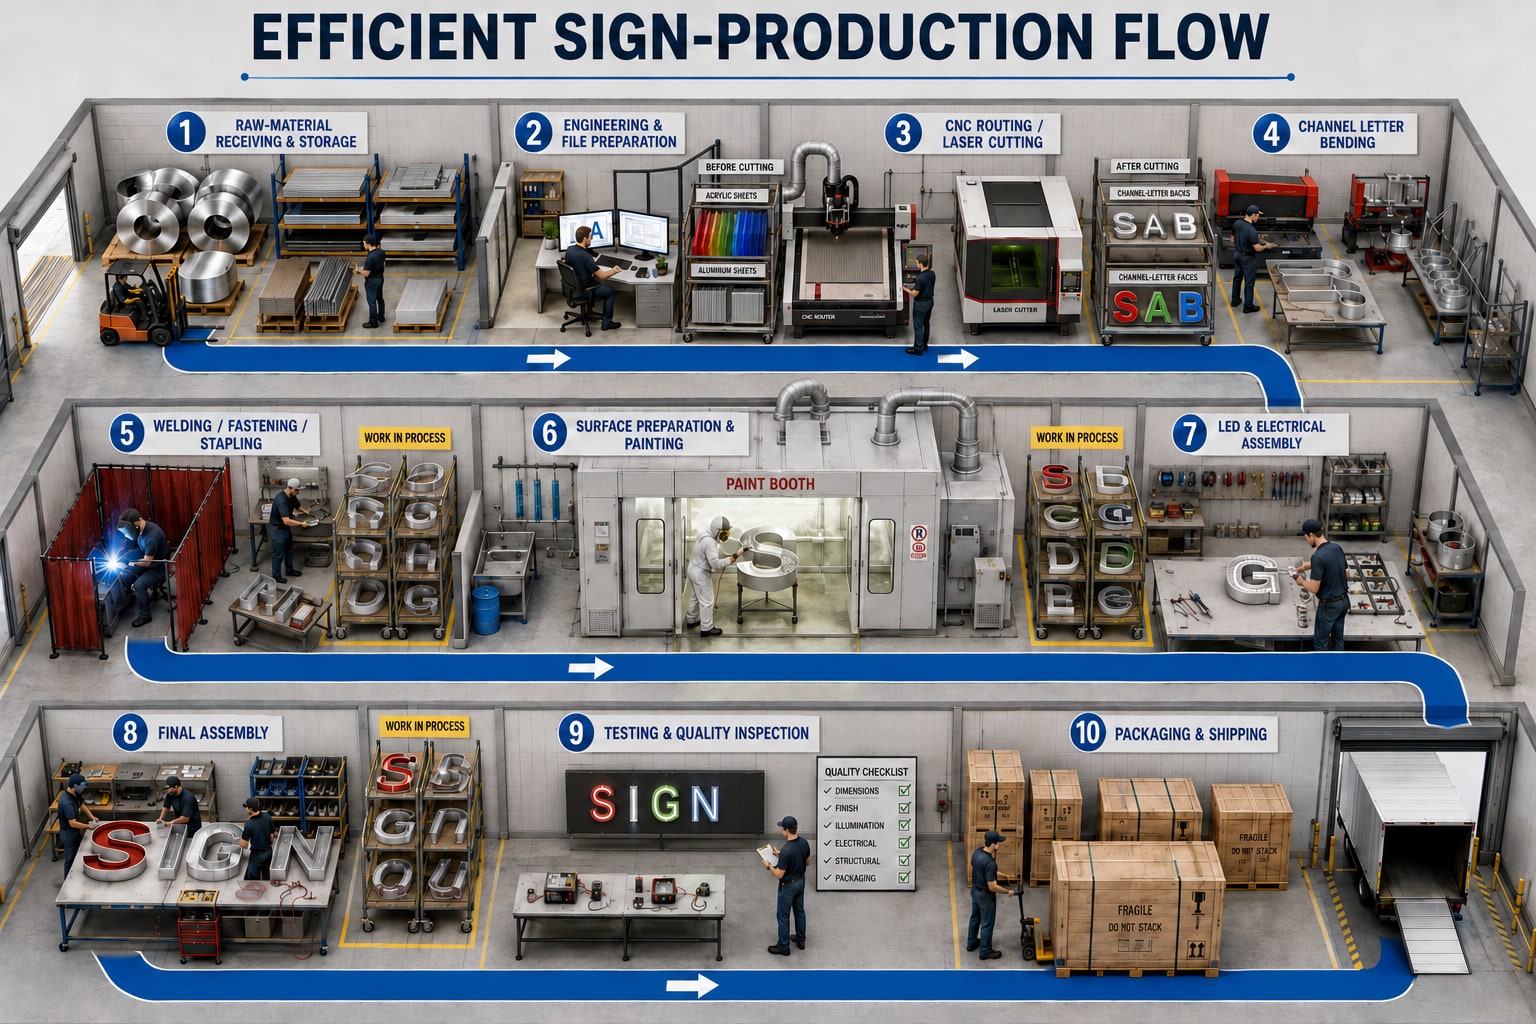
Here's a channel-letter workflow Canadian and U.S. shops adopt quickly:
1. Vector prep with kerf in mind
- Expand strokes; keep paths clean.
- Add 0.05–0.2 mm kerf offset test swatches to dial fit between faces and returns.
2. Nesting for yield
- Group letters by material and thickness.
- Use tight common-line nesting on straight runs to reduce scrap by 8–15%.
- Keep grain direction consistent on brushed plastics.
3. Focus and air assist
- A slight defocus (+0.2–0.5 mm) on thicker acrylic can smooth the edges.
- Moderate air assist helps avoid haze while keeping flames at bay.
4. Edge quality check
- Cut a sample "O" and "A" for every new sheet lot.
- Note the speed/power that keeps inside corners clear.
5. Assembly jigs
- Laser-cut simple MDF or acrylic jigs with alignment marks for repeat SKUs.
- Add engraved labels to each jig—no more mystery pieces.
Good nesting and kerf calibration shorten the time to the first usable part. On-site setup also lets the operator learn these adjustments using the shop's own files and material.
Advice from the best CNC Laser Cutter Manufacturers: Laser vs. router for faces and backs
When does the Acrylic Laser Cutter win?
- Small text and tight geometry: No bit deflection, no tool-diameter limits.
- Edge finish: Often glossy right off the bed; no flame pass required.
- Noise and dust: You're dealing with fume extraction rather than chips everywhere.
- Throughput on thin plastics: One pass, consistent speed.
When might a router still be a good choice?
- Very thick plastics (beyond your preferred laser range).
- Metals (unless you're marking coated material).
- Dimensional bevels that rely on special bits.
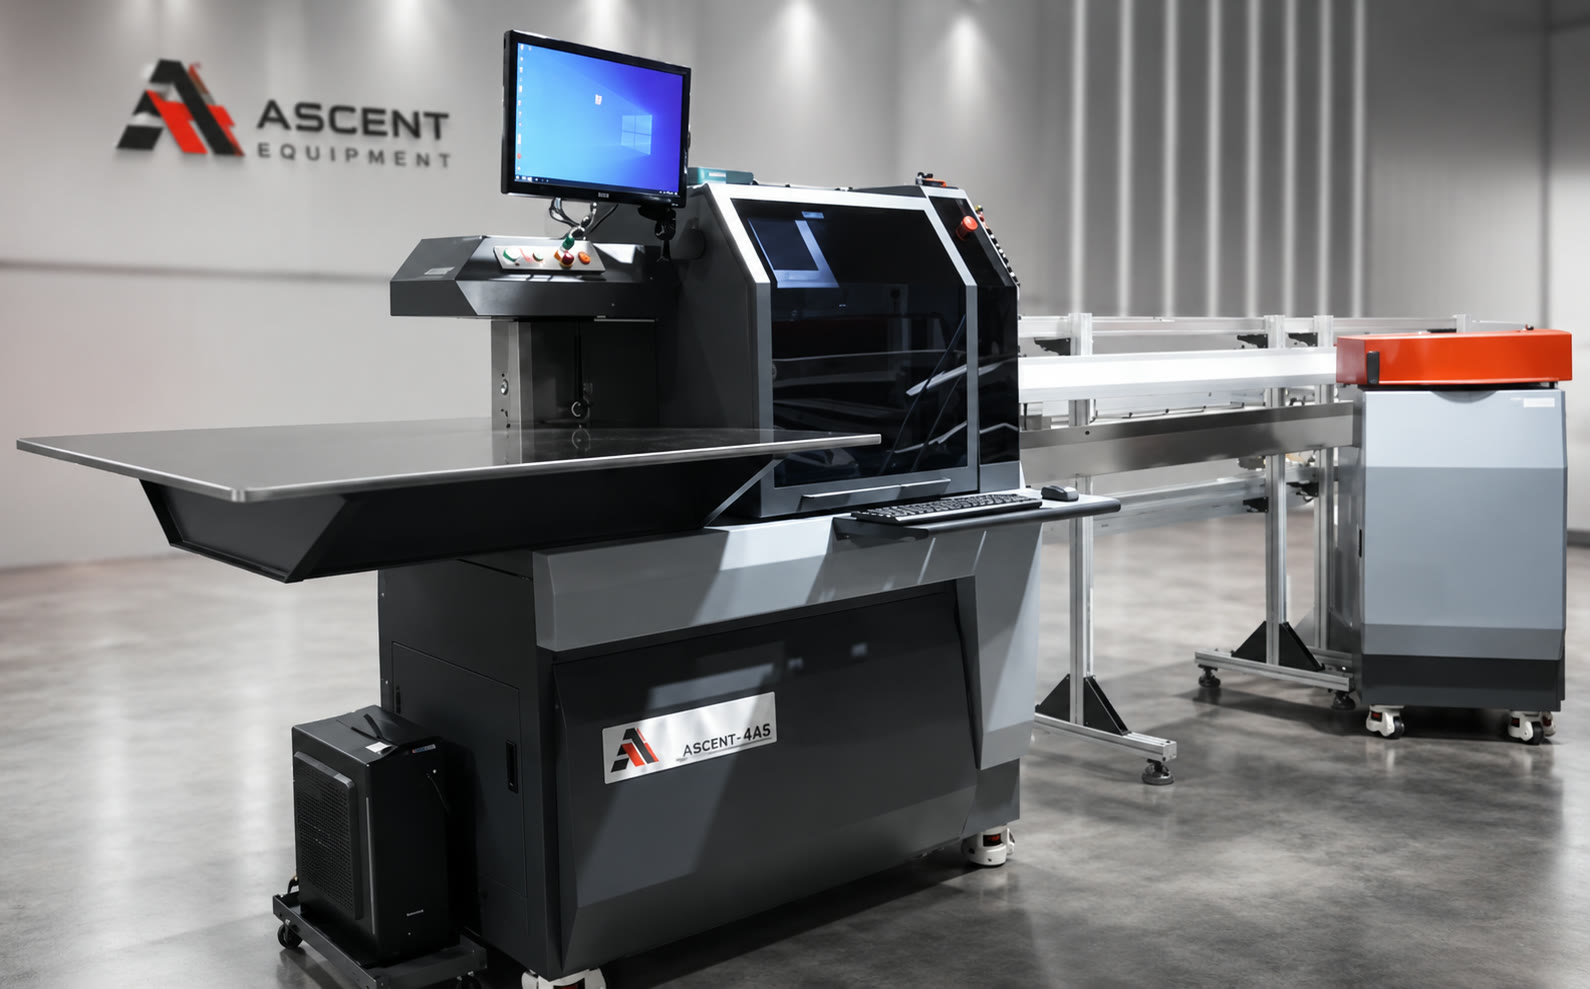
Many CNC laser cutter manufacturers recommend a hybrid cell: a laser for faces/backs, and a router for special-case substrates. If you're in Canada & USA, this split keeps your capital investment reasonable while raising overall shop capacity.
Practical ventilation and winter tips (Canada & USA)
Cold weather and long duct runs can cause condensation inside vent lines. A few shop-friendly moves:
- Shorter, insulated runs to the outside reduce vapor and odor.
- An inline fan downstream of the laser keeps negative pressure through the entire path.
- Condensate traps at low points stop drips from reaching the machine.
- Regular pre-filter changes keep airflow strong when you're cutting acrylic daily.
These tweaks matter for shops across Canada & USA, especially in winter when doors stay shut and makeup air is limited.
Simple pricing model you can steal
Use this quick, defensible way to quote laser-cut faces/backs:
- Machine time: (Cut length + pierce count + engraving time) × shop rate.
- Material: Sheet cost ÷ yield (based on your nesting).
- Overhead: A small per-part charge for lenses, filters, and tape.
- Assembly add-ons: Mounting holes, diffuser layers, and QA checks.
Clear line items make repeat quotes easier to defend. Customers can see what they are paying for when the edge finish and fit are consistent.
Lesser-known tricks that boost finish quality
- Mask the top surface with paper or a poly mask to avoid micro-marring; peel it after cutting.
- Start points: Place them in inconspicuous corners; reduce dwell time at the start to prevent witness marks.
- Lead-ins/lead-outs: Tiny tangential moves can smooth transitions on sharp inside corners.
- Beam alignment checks weekly: Two minutes, big payoffs in cut consistency.
- Use a fine-to-coarse test grid to quickly lock in speed/power for new acrylic brands.
Subtle clouding on the edge often points to dirty optics or too much air assist. Clean the lens and test a small airflow adjustment before changing the rest of the cut settings.
Installation, training, and support that actually show up
A new machine only becomes useful when the team can run real jobs on it. Ascent Equipment handles installation, setup, and hands-on training at your facility in Canada or the USA. That means:
- Your team learns real jobs on your files.
- Calibration and maintenance are covered step-by-step.
- You get a 1-year warranty on non-consumable parts and workmanship, plus approachable techs when you need help.
Plenty of machines look similar on paper. The difference is how quickly you're making sellable parts—and whether the support is a real person on your floor, not a ticket thread in another time zone.
Quick self-check: Is a 130W Acrylic Laser Cutter right for you?
- Do you cut 3–6 mm acrylic faces/backs weekly?
- Are you spending hours hand-finishing router edges?
- Do you want local install and training in Canada & USA?
- Would faster nesting and clean edges help you ship more channel letters each month?
If most of those points describe your workload, a 130W Acrylic Laser Cutter is worth comparing with the labor and finishing cost of your current process.
Ready to make channel letters easier?
A 130W Acrylic Laser Cutter gives a channel letter shop clean acrylic edges and repeatable cycles without adding another manual finishing step. Ascent provides installation, training, and warranty coverage in Canada and the USA.
Contact Ascent Equipment to review the acrylic sizes and thicknesses in your channel letter lineup and confirm whether 130W is the right fit.